Introduction
In today’s era of the Internet of Everything, traditional manufacturing is undergoing a profound digital transformation. From static assembly lines to dynamic data-driven factories, companies increasingly combine RFID technology with Internet of Things (IoT) platforms to realize real-time awareness and intelligent management of assets, inventory, people and production processes. This trend is reshaping manufacturing standards and heralding the era of “Standard Manufacturing 2.0”.
1. Why combine RFID with IoT?
Challenges of traditional manufacturing
| Problem Type | Description |
| Slow data collection | Relying on manual operation or barcode scanning, low efficiency, lagging update |
| Siloed information | The data of each link is scattered, lack of unified platform integration |
| High error rate | Manual records or scanning operations are prone to errors, increasing rework and costs |
| Lack of traceability | Unable to track the status and flow path of products in the manufacturing process |
| Non-transparent management | Lack of real-time feedback mechanism, difficult to detect and respond to abnormal problems in a timely manner |
The Core Value of RFID + IoT
| Advantage | Description |
| Real-time data collection | RFID labels can upload real-time location information, status changes and usage frequency, reducing human intervention |
| Full Life-cycle Management | Tracks the entire process from raw material procurement, production, warehousing to shipment |
| Cost Reduction and Efficiency | Reduces human error, optimizes resource allocation and improves overall operational efficiency |
| Increase transparency and compliance | Meet the traceability and compliance needs of medical, food, automotive and other industries |
| Intelligent Prediction and Analysis | The IoT system aggregates data from multiple sources and supports AI analysis, predictive maintenance and early warning mechanisms |
2. Six application scenarios of RFID+IoT

Intelligent identification and traceability of raw materials
Each batch of raw materials is labeled with RFID labels, which automatically record the time of entry, supplier, and testing information.
The system automatically verifies whether the material specifications match the purchase order;
The system automatically verifies whether the material specification matches the purchase order;
System warning: prevent expiration or misuse.
Intelligent production line tracking
Whenever a work-piece completes a process on the production line, the RFID reader automatically records its status.
Realize precise beat management and bottleneck identification;
Process abnormality automatic reminder, support traceability improvement;
Flexible scheduling and dynamic allocation of production resources.
Equipment and Mold Management
Attach high-temperature RFID labels to key equipment and moulds to achieve life cycle management.
Real-time monitoring of the frequency of use, and maintenance status;
Automatically determine the life warning and scrap reminder;
Reduce the risk of downtime due to unknown equipment status.
Warehouse logistics automation
RFID antenna covers the whole warehouse area, realizing the automatic warehousing, inventory and discharge of goods.
Replaces manual code scanning, increasing efficiency by more than 3 times;
Automatically trigger the WMS system to update inventory status;
Linkage with AGV trolley to realize unmanned handling.
Security and Permission Control
Employees enter the workshop through RFID work labels, and the system automatically recognizes their authority and operation history.
Restrict the operation authority of high-risk equipment;
Abnormal departure alarm, dangerous area access control;
Linkage of face recognition, video monitoring system.
Environment and Energy Consumption Supervision
Cooperate with IoT sensors to dynamically record production environment and equipment energy consumption data.
Temperature and humidity abnormal automatic alarm;
Energy data statistics analysis to support energy saving and emission reduction;
Green manufacturing assessment basis.
3. The core of Standard Manufacturing 2.0: data-driven + precision control
Standard Manufacturing 2.0 is not just a hardware upgrade, but a transformation logic driven by data at its core.
A closed loop of data-driven logic
Data collection layer: RFID provides object identification and tracking, IoT sensors provide environment and state sensing;
Data transmission layer: Edge gateway, 5G communication, and MQTT protocol guarantee safe and stable data transmission;
Data processing layer: cloud platform/private cloud real-time computing to build digital twin factories;
Application execution layer: the system automatically issues scheduling instructions to drive actual process changes.
Five aspects of precise control
Production beat control: Adjust equipment movement and beat frequency based on RFID real-time work piece position;
Quality process control: combining RFID tracking and sensing data to identify abnormal batches, realizing fast quality closed loop;
Precise inventory control: real-time inventory visualization, support JIT / Kanban replenishment;
Equipment energy consumption control: analysis of equipment operation status and power data to optimize power consumption strategy;
Planning and scheduling control: The IoT platform combines historical data and AI forecasts to dynamically optimize capacity load and order priority.
Leap from Automation to Intelligence
Automation emphasizes “execution instead of manpower”, while intelligence emphasizes “decision optimization process”;
RFID+IoT realizes the closed loop of the perception layer, which provides a high-quality database for AI;
Supporting advanced manufacturing capabilities such as predictive maintenance, adaptive scheduling and self-healing from abnormalities.
4. Typical industry case studies
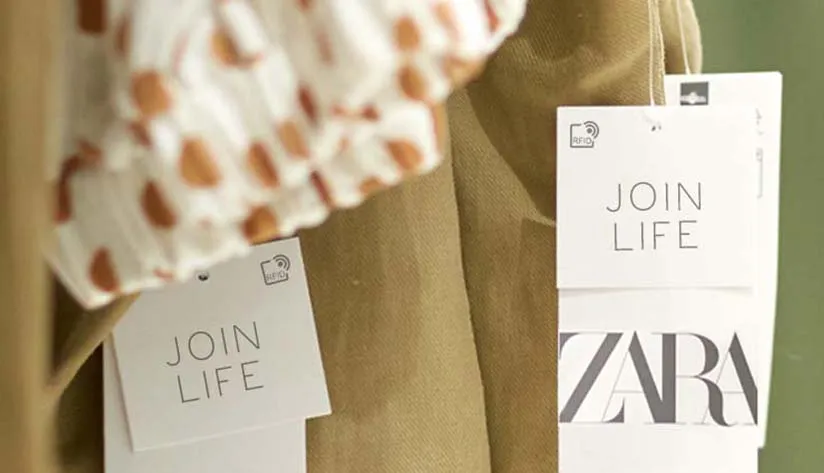
Apparel Manufacturing: Zara Uses RFID Tagging System
Challenge: Zara has a large number of stores around the world and many SKUs, making it difficult for traditional barcodes to support efficient warehousing and store replenishment needs.
Solution: Zara uses UHF RFID labels for clothing, hang tags, and packaging, and deploys supporting readers.
Results: Inventory accuracy increased from 85% to 98%; store staff inventory time was reduced by 70%; store replenishment response accelerated.
Automotive Parts Manufacturer: Introducing RFID to Track Parts Life–cycle
Challenge: The variety of parts makes quality traceability difficult.
Solution: Each part is labeled with a high-temperature resistant RFID label to record the entire process from manufacturing, testing to shipping.
Result: Traceability of quality issues, increased customer satisfaction, and reduced recall costs.
Electronics Manufacturer: Supporting Apple’s third-party factory to realize accurate material management
Challenge: Fast production pace, frequent material turnover, prone to material errors and leakage.
Solution: Use customized metal-resistant RFID labels and supporting industrial readers, combined with MES system application.
Result: Reduce the rate of wrong materials by 90%, and improve the efficiency of warehousing by 2 times.
Intelligent access control manufacturer: European subway system using RFID cards
Challenge: High demand for subway passes, high life expectancy and anti-counterfeiting performance need to be strengthened.
Solution: NXP chip RFID cards, support for data encryption, and secure authentication, can prevent copying and imitation.
Result: Improved security level, accelerated access efficiency, and a significant increase in passenger satisfaction.
Conclusion
Manufacturing into the intelligent today, RFID and the combination of the Internet of Things is no longer a future trend, but now the enterprise should grasp the transformation opportunities. Through the introduction of these technologies, enterprises can not only improve operational efficiency but also enhance product traceability and brand value. The core of Standard Manufacturing 2.0 is data, and RFID is the key weapon to obtain these data.
As an enterprise focusing on RFID product manufacturing and exporting, RFIDLabel will continue to provide customers with high-quality, customized, environmentally friendly RFID solutions to help global manufacturing enterprises into a new era of real-time intelligent management.
Recommended Product